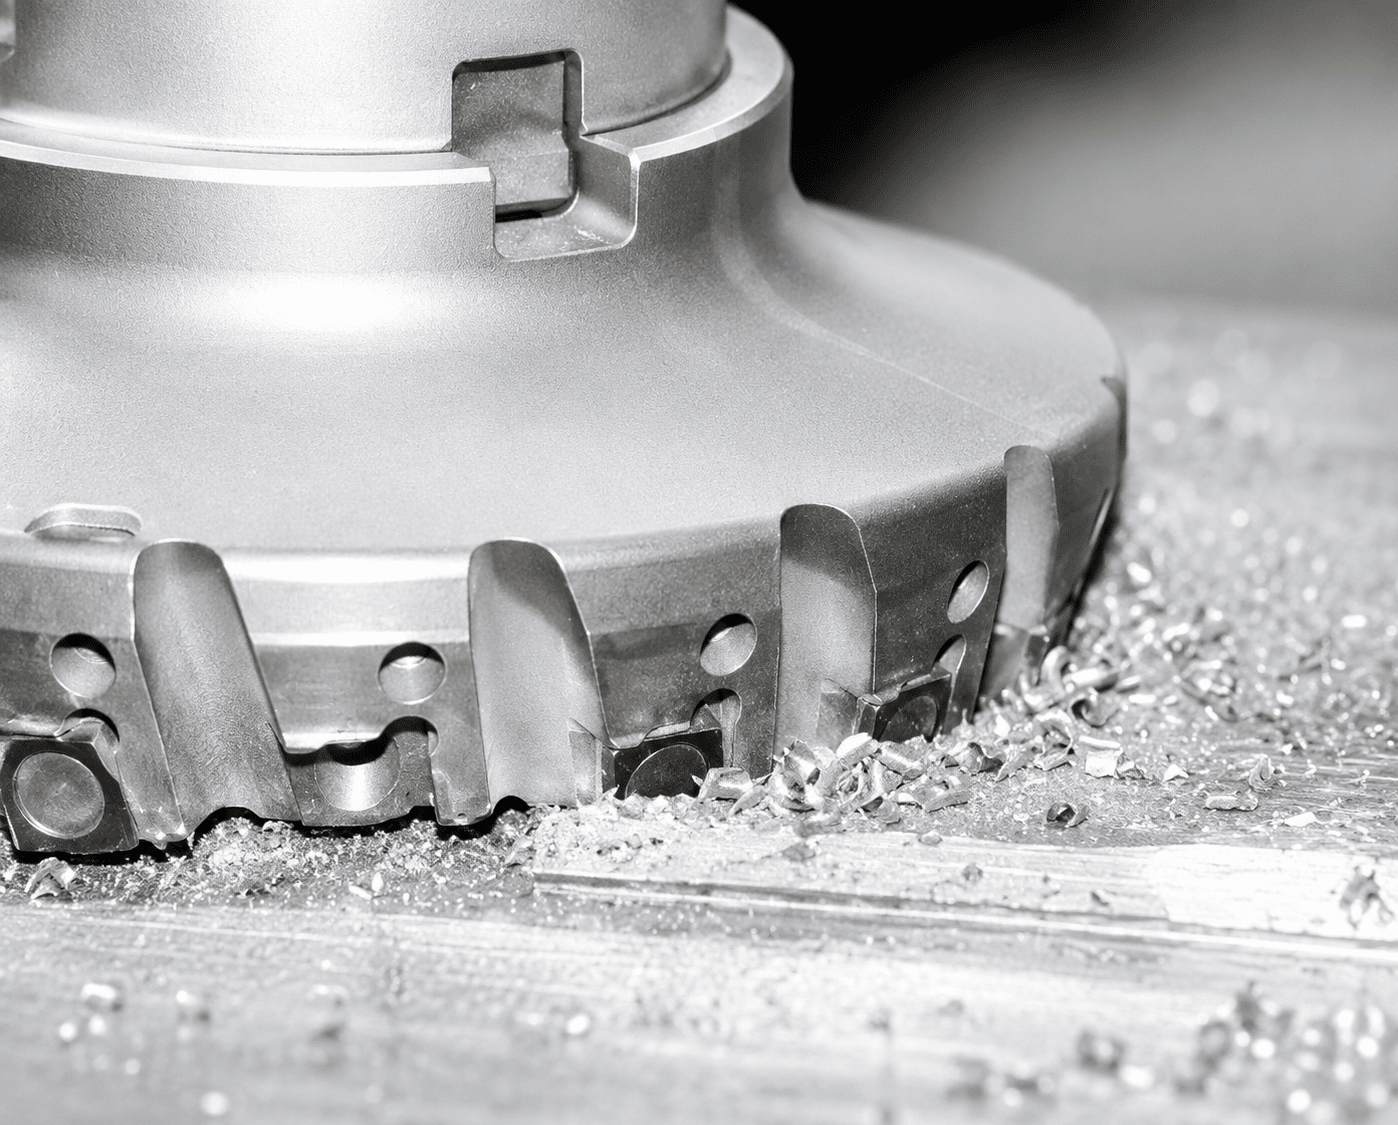
Despite a titanium carbide content of approximately 45 vol.-% and an annealed hardness of 48–53 HRC, Ferro-Titanit® is machinable by known cutting methods. The key factors are reduced cutting speeds compared with steel – and always dry machining.
Turning, Milling, Drilling, Thread Cutting, Sawing
Ferro-Titanit® is machinable by all common cutting processes. Key rule: significantly reduce cutting speeds compared with steel, always machine dry – no coolant.
Turning
| Ferro-Titanit® grades | Tooling (alternative) | Feed | Cutting edge angles | vc m/min |
||
|---|---|---|---|---|---|---|
| Rake angle |
Inclination angle |
Clearance angle |
||||
| C-Spezial | Carbide, coated K 10 / K 30, HSS (no coolant) |
0,02–0,1 mm/U | 6° / 15° | 0° / −6° | 6° / −11° | 10 |
| WFN | 8 | |||||
| S | 8 | |||||
| NIKRO 143 | 5 | |||||
| NIKRO 128 | 5 | |||||
| U | 5 | |||||
| CROMONI | 0,02–0,04 mm/U | 2,5 | ||||
| all grades | Ceramic / fibre-reinforced | ~0,1–0,5 mm/U | −6° | −6° | +6° | > 25 |
ℹ Dry machining – do not use coolant.
Milling
| Ferro-Titanit® grades | Tooling (alternative) | Feed | vc m/min |
|---|---|---|---|
| C-Spezial | Carbide, coated K 10 / K 30, HSS |
0.01–0.07 mm/tooth | 6–12 |
| WFN | |||
| S | |||
| NIKRO 143 | |||
| NIKRO 128 | |||
| U | |||
| CROMONI | ~0,01 mm/Zahn | 2–5 |
Drilling
| Ferro-Titanit® grades | Tooling (alternative) | Feed | vc m/min |
|
|---|---|---|---|---|
| all grades | Carbide, coated K 10 / K 30, HSS |
0,05 mm/U | Point angle 90–120° | 2–4 |
Thread Cutting
| Ferro-Titanit® grades | Tooling (alternative) | Feed | Rake angle | vc m/min |
|---|---|---|---|---|
| all grades | HSS, Carbide |
0 Chamfer 1.5–2 mm wide, strong back relief |
2–4 |
Sawing *
| Ferro-Titanit® grades | Tooling (alternative) | Feed | Constant a for feed calculation | vc m/min |
|---|---|---|---|---|
| C-Spezial | Bi-metal M 42 | Constant a Length of cut |
800 mm²/min | ~10 |
| WFN | ||||
| S | ||||
| NIKRO 143 | 600 mm²/min | |||
| NIKRO 128 | ||||
| U | ||||
| CROMONI | 200 mm²/min | < 5 |
* Band saw (preferred); hacksaw (in exceptional cases)
Recommended blade pitch by cross-section
| Cross-section to be cut | Standard pitch | Combi pitch |
|---|---|---|
| bis 30 mm | 10 ZpZ | 8/12 ZpZ |
| 30–70 mm | 8 ZpZ | 5/8 ZpZ |
| 70–120 mm | 4 ZpZ | 4/6 ZpZ |
| > 120 mm | 3 ZpZ | 2/3 ZpZ |
ℹ Band saw (preferred) · Hacksaw (in exceptional cases)
Tolerances and surface finish
The high carbide content and hardness of the titanium carbides require particular care during grinding. Recommended grinding wheels depend on the condition of the material.
Soft-annealed condition
Corundum wheels with ceramic bond, porous structure and fine grain
Hardened condition
Diamond wheels from nickel-coated synthetic diamonds in resin bond – especially recommended for finish grinding
Diamond wheel parameters
| Parameter | Recommendation |
|---|---|
| Diamantkonzentration | 75c – 100c |
| Körngröße | D 107 – D 151 |
Basic rules
Apply a strong coolant jet close to the contact zone
Use small infeed increments
Optimum surface finish
For high-quality Ferro-Titanit® materials, surface finish is critical for the service life of tools and machine parts. After grinding, polishing with diamond polishing paste is recommended.
Grain 10–25 μm
Diamond polishing paste
Grain 2–5 μm
Diamond polishing paste
Grain 1–2 μm
High-gloss finishing
ℹ Well-polished tools significantly minimise cold-welding tendency in service.
Realising complex geometries
EDM allows geometries to be realised that are difficult to access by cutting – ideal for intricate tool contours. Ferro-Titanit® hard phases are subject to the same influences as tool steels and hard metal.
ℹ After EDM, reworking and a stress-relief treatment must be carried out to reduce surface stresses caused by the recast layer.
Recommended procedure
Rough EDM
Remove rough contour with low pulse energy
Semi-finish EDM
Finish to accurate final contour
Finish EDM
Fine-finish surface for best quality
Stress-relief treatment
Reworking and stress relief after EDM
Data sheets with grade-specific reference values
Detailed machining guidelines for each Ferro-Titanit® grade are contained in the material data sheets. Available on request.